-
E-mail
ouyangchao@qh-ndt.com
-
Phone
15275259479
-
Address
No. 12, Lane 555 Tianzhu Road, Jiading District, Shanghai, 2004
Product Categories
Qianhu Testing (Shanghai) Co., Ltd



Phased array flaw detector
NegotiableUpdate on 01/23
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
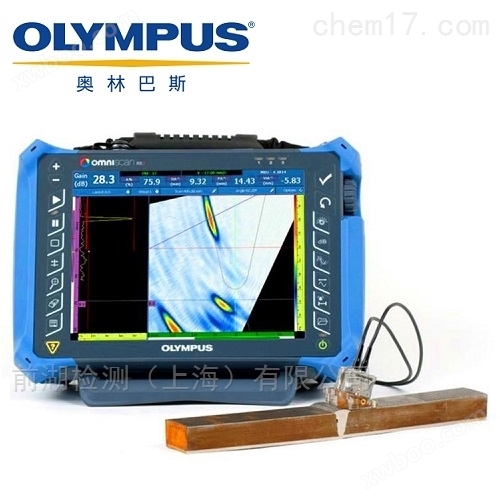
Olympus Omniscan MX2 phased array flaw detector is used to detect defects such as cracks, slag inclusions, porosity, and looseness in welds, pipes, bars, plates, forgings, and castings.
Product Details
OlympusPhased array flaw detectorOmniscanMX2Used for detecting defects such as cracks, slag inclusions, porosity, and looseness in welds, pipes, bars, plates, forgings, and castings.
For over a decade, Olympus has been the industry leader in developing modular NDT testing platforms. Its OmniScan MX is the most successful portable, modular phased array testing instrument to date, with thousands of OmniScan MX instruments in use around the world.
Now, Olympus has launched a new phased array module using TOFD technology, a new UT module, and new software programs (NDT Setup Builder and new version OmniPC), which expand the performance of the already successful OmniScan MX2 platform and improve the efficiency of non-destructive testing workflows.
Solid foundationThe OmniScan MX2, a second-generation instrument, is not only compatible with over 10 phased array and ultrasound modules, but also improves detection efficiency: its faster setup speed, shorter detection cycle, and faster report creation characteristics ensure high-level application of advanced AUT. This upgradable testing platform developed for NDT experts can achieve true next-generation NDT testing in the future. The OmniScan MX2, a portable and modular instrument, not only has a high acquisition rate, but also adds a variety of powerful software functions, making manual and automatic detection more effective. |
|

Faster and better!With the OmniScan MX2 instrument, your work will be more awesome! The OmniScan MX2 instrument features a highly intuitive step-by-step guide that simplifies and accelerates the setup process, allowing users to quickly begin testing. This MX2 instrument is equipped with a wider and brighter 10.4-inch (26.4 cm) screen, featuring a modern, * *, and intuitive touchscreen function. Its phased array user interface, which meets industry standards, responds faster and transmits data faster than ever before, allowing users to start the next test more quickly. |
 |
Not only an ordinary instrument, but also the core of the detection solution
OmniScan MX2 is an important part of the detection solution, combined with other critical components to form a complete detection system. Olympus can provide a complete range of testing products, including phased array probes, scanners, analysis software, and various accessories. These products can be integrated and packaged according to specific application requirements, becoming solution packages that can be quickly assembled together for a particular application. Users can receive a quick return on investment in purchasing the product. In addition, Olympus provides high-quality calibration and maintenance services worldwide, and its expert team proficient in phased array applications ensures that customers can receive immediate technical support when they need assistance.
 |
 |
 |
 |
|
Welding seam inspection of pressure vessels Users can use an OmniScan PA and a manual scanner such as the HSMT series, or an electric scanner such as WeldROVER, to conduct a complete inspection of the welds of pressure vessels through a single scan. If TOFD and PA are combined in a single detection process, it will greatly reduce detection time compared to conventional grating scanning or radiographic imaging techniques. In addition, users can also receive real-time detection results, so that they can discover problems related to welding equipment at any time and solve them immediately. |
Composite material testing Due to the various shapes and thicknesses of workpieces made from laminated composite materials, the inspection of these workpieces can be considered a challenge. Olympus provides a complete solution for the structural testing of carbon fiber reinforced polymer materials. These solutions are based on OmniScan flaw detectors, GLIDER scanners, as well as probes and wedges specifically designed for CFRP flat and curved surface inspection. |
Welding seam inspection of small diameter pipe fittings When used with the COBRA manual scanner, the OmniScan flaw detector can detect pipe fittings with an outer diameter range of 0.84 inches to 4.5 inches. The appearance of this manual scanner is very narrow, so it can enter narrow spaces to inspect pipelines. The distance between the tested pipe and its surrounding objects, such as pipes, brackets, or frames, can be as small as 12 millimeters (0.5 inches). |
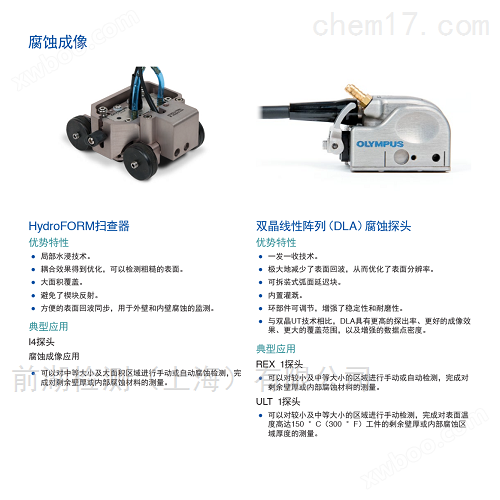
Manual and semi-automatic corrosion imaging The purpose of using the OmniScan PA system in conjunction with the HydroFORM scanner is to provide a detection solution for detecting wall thickness reduction caused by corrosion, abrasion, and erosion. In addition, this system can also detect wall damage, such as hydrogen induced foaming or delamination generated during the manufacturing process, and can clearly distinguish these abnormal phenomena from wall thickness reduction. In this application, phased array ultrasound technology has the characteristics of fast detection speed, appropriate data point density, and high detection level. |
Modular Instrument
Continuous demand updates and platform innovation
In the process of designing the OmniScan MX2 instrument, we took into account the current and future investment returns of users in phased array technology, so this instrument can be equipped with more than 10 different Olympus modules. The technical specifications of the instrument will be continuously developed and improved through software updates to meet the needs of users, ensuring a significant return on investment for users.
PA2 and UT2 modules
As a company in the phased array technology industry, Olympus has just launched a new module series compatible with MX2 instruments.
|
PA2 The new phased array module series, represented by the innovative PA2 module, has improved performance in many aspects, such as: Excellent phased array and TOFD signal quality to date
Improved multiple sets of performance
Improvement of general hardware specifications
|
 PA216:64 PA2 16:128 PA2 32:128 PA2 32:128PR |
|
UT2 The new UT2 conventional ultrasound module has the same technical performance as the UT channel of the PA2 module, but its UT channel is twice that of the PA2 module. |
 Dual channel UT2 |
The new OmniScan software enhances the functionality and performance of weld and corrosion detection applications.
In order to achieve the goal of continuous improvement, the software interface has been simplified and response time has been optimized, allowing users to experience the most efficient detection process possible.
The newly added features are as follows:
- Export C-scan
- New end view with group fusion function
- Interlocking function
- Attenuation gain in analysis mode
- Rolling layout facilitates the reading process
- Provide more interactive menus to improve access capabilities
- Optimized main menu and wizard obtained
- Airborne composite fan scanning function
- Surface geometry acoustic ray tracking for longitudinal weld seam detection
- Phased array DGS/AVG function, can be used for all focusing rules with S-scan image correction

For applications that require the use of multiple probe configurations, the multi group layout has been improved, and the improved layout can reflect the scanner configuration in the software interface. The different scanning positions are determined by their distance from the center of the weld seam, providing a layout that is both easy to understand and visually appealing.
OmniScan product series
|
design NDT SetupBuilder Your needs collect OmniScan Data analysis and report production OmniPC TomoView The performance of TomoView is as follows:
|
 |
Design using NDT Setup Builder
Collect data using OmniScan MX2
Using OmniPC for analysis
Design using NDT Setup Builder
|
NDT Setup Builder is a newly developed software based on PC, which helps to create detection settings and display simulated images of sound beams. This software has multiple functions and can easily and quickly develop comprehensive testing plans, which can be directly imported into the OmniScan MX2 instrument.
|
|

Set up using OmniScan MX2 instrument
|
The effective method for creating settings is to simulate them in NDT Setup Builder and then import them directly into OmniScan through an SD card or USB key. Before collecting, only a few basic operations need to be performed in the instrument, such as setting the gate and range. Due to the following features of OmniScan, users can also easily create settings in the instrument:
|
|

Collect data using OmniScan MX2
Thanks to the use of NDT Setup Builder and OmniPC software, the OmniScan MX2 is able to perform calibration and acquisition operations. However, if users are willing, they can also complete all the steps of the inspection directly on the convenient and large touch screen of OmniScan. |
|

calibration
To complete a standardized inspection, the calibration wizard in the instrument ensures that each focusing rule in each group is directly equivalent to a single channel conventional flaw detector. Users will receive step-by-step guidance from the wizard during the required calibration process. The calibrated items include sound velocity, wedge delay, sensitivity, TCG, DAC, AWS, and encoder. Now, the instrument can automatically perform TOFD PCS calibration and straight wave straightening operations.
collect
The OmniScan MX2 allows for easy configuration of detection parameters during manual, single line, or raster encoded scanning. The collected data can be displayed in real-time on the screen in different viewing formats, and users can also store the data in SD cards or USB 2.0 devices with hot swappable functions.
- Intelligent layout, configurable up to 8 groups
- Full screen mode can better display defects
- Different combinations of gates can be used to process synchronization and measurement
Using OmniPC for data analysis
|
OmniPC is a new software program that not only has the same user interface, analysis capabilities, and reporting capabilities as OmniScan, but also has greater flexibility to run on personal computers. By using OmniPC, the OmniScan instrument can perform centralized scanning operations, and users can analyze the collected data on their personal computers. This software can also be used with a large screen to improve image visibility, and the shortcuts on the computer keyboard make operations faster. |
|

Using OmniScan MX2 for data analysis
- The data cursor, reference cursor, and measurement cursor are used for the quantification of defects.
- Expanded database, pre-defined list of trigonometric parameters, statistical data of defects relative to the axis, volume position information, qualification standards based on specifications, and statistical data of corrosion imaging, etc.
- During the offline gate repositioning operation, views can be linked together for interactive analysis and automatic updates.
- The optimized preset layout can quickly and conveniently quantify the length, depth, and height of defects.
Report production
Both OmniScan MX2 and OmniPC can generate reports containing defect reports. The defect report can list up to 8 readings, such as wave amplitude, position, and defect size. Users can customize the report according to their needs, add more readings, add comments for each defect indication, and save the report as an HTML file. The RayTracing tool can indicate the location of defect indications in the weld profile. High resolution images can be inserted into all relevant detection parameters.
Compatibility of OmniScan MX2 software
| module | OmniScan airborne data acquisition |
OmniScan controlled by TomoView |
Equipped with analysis software |
| UT | MXU 4.3R2 | TomoView 2.10R19 with OSTV PA1 3.0R9 | OmniPC 4.3R2 |
| TomoView 2.10R19 | |||
| PA | MXU 4.3R2 | TomoView 2.10R19 with OSTV PA1 3.098 | OmniPC 4.3R2 |
| TomoView 2.10R19 | |||
| UT2 | MXU 4.3R2 | TomoView 2.10R19 | OmniPC 4.3R2 |
| TomoView 2.10R19 | |||
| PA2 | MXU 4.3R2 | TomoView 2.10R19 with OSTV PA2 1.0R2 | OmniPC 4.3R2 |
| TomoView 2.10R19 |
Please note that files generated by previous software versions are supported by the released versions.
OlympusPhased array flaw detectorOmniscanMX2
Technical specifications of OmniScan MX2 host
| General specifications | External dimensions (width x height x thickness) | 325 mm x 235 mm x 130 mm (12.8 in. x 9.3 in. x 5.1 in.) |
|---|---|---|
General specifications |
weight | 3.2 kilograms, without module, with one battery. |
| data storage | storage device | SDHC card, most standard USB storage devices, or Fast Ethernet* *To obtain results, it is recommended to use Lexar ® Memory card. |
data storage |
Data file capacity | 300 MB |
| I/O port | USB port | 3 of them |
I/O port |
Audio alarm | yes |
I/O port |
video output | Video Output (SVGA) |
I/O port |
Ethernet | 10/100 Mbps |
| Input/output cable | encoder | Dual axis encoder line (orthogonal, upward, downward, or clock/direction) |
Input/output cable |
digital input | 4 digital TTL inputs, 5V |
Input/output cable |
digital output | 4 digital TTL outputs, 5 V, 15 mA |
Input/output cable |
Collection opening/closing device | Remote acquisition start TTL, 5V |
Input/output cable |
Power output line | 5 V, 500 mA power output line (with short circuit protection) |
Input/output cable |
call the police | 3 TTL,5 V,15 mA |
Input/output cable |
analog output | 2 analog outputs (12 bits), ± 5 V, 10 k Ω |
Input/output cable |
Step speed input | 5 V TTL pace input |
| display | display size | 26.4 cm (10.4 inches) (diagonal) |
display |
resolution | 800 x 600 pixels |
display |
brightness | 700 cd/m2 |
display |
number of colors | 16 million |
display |
type | Thin film transistor liquid crystal display (TFT LCD) |
| power supply | Battery Type | Intelligent lithium-ion battery |
power supply |
Number of batteries | 1 or 2 batteries (two hot swappable batteries can be accommodated in the battery compartment) |
power supply |
Battery power supply time | Using two batteries saves 7 hours |
| environmental indicators | Working temperature range | -10 °C~45 °C (14 ºF~113 ºF) |
environmental indicators |
Storage temperature range | -20 ° C to 60 ° C (-4 ° F to 140 ° F), with battery -20 ° C to 70 ° C, without battery |
environmental indicators |
relative humidity | Under non condensing conditions at 45 ° C, the high relative humidity is 70%. |
environmental indicators |
Intrusion protection rating | Designed to meet IP66 rating |
environmental indicators |
Anti collision rating | Through the drop test of MIL-STD-810G 516.6 |
| Compatibility of MX2 module | MXU 4.1R8 and updated versions | OMNI-M2-PA32128PR |
Compatibility of MX2 module |
MXU 4.0 and later versions | OMNI-M2-PA1664 |
Compatibility of MX2 module |
MXU 4.0 and later versions |
OMNI-M2-PA16128 |
Compatibility of MX2 module |
MXU 4.0 and later versions |
OMNI-M2-PA32128 |
Compatibility of MX2 module |
MXU 4.0 and later versions |
OMNI-M2-UT-2CH |
Compatibility of MX2 module |
MXU 3.1 and MXU 4.1R9 and updated versions | OMNI-M-UT-8CH |
The OmniScan MX2 meets or exceeds the requirements for instruments and software specified in ASME, AWS, API, and EN specifications.
Technical specifications of phased array module (applicable to OMNI-M2 module)
| General specifications | External dimensions (width x height x thickness) | 226 mm x 183 mm x 40 mm (8.9 in. x 7.2 in. x 1.6 in.) |
|---|---|---|
General specifications |
weight | 1.6 kg(3.5 lb) |
General specifications |
interface | 1 phased array interface: Olympus PA interface 2 UT interfaces: LEMO 00 |
General specifications |
Number of focusing rules | 256 pieces |
General specifications |
probe identification | Automatic probe recognition |
| Pulse generator/receiver | aperture | 32 chips* |
Pulse generator/receiver |
Number of chips | 128 chips* |
| pulse generator | PA channel | UT channel |
| voltage | 40 V、80 V、115 V | 95 V、175 V、340 V |
| pulse width | Adjustable from 30 ns to 500 ns, with a resolution of 2.5 ns. | Adjustable within the range of 30 ns to 1000 ns, with a resolution of 2.5 ns. |
| Pulse shape | Negative square wave | Negative square wave |
| output impedance | < 25 Ω | < 30 Ω |
| receiver | PA channel | UT channel |
| gain | 0 dB~80 dB, The large input signal is 550 mVp-p (full screen height) | 0 dB~120 dB, The large input signal is 34.5 Vp-p (full screen height) |
| input impedance | 65 Ω | Pulse echo mode: 60 Ω Pulse transmission and reception mode: 50 Ω |
| System bandwidth | 0.6 MHz~18 MHz(–3 dB) | 0.25 MHz~28 MHz(–3 dB) |
| Sound beam formation | Scan type | Fan shaped and linear |
|---|---|---|
Sound beam formation |
number of groups | 8 more |
| data collection | Digital frequency | 100 MHz |
data collection |
High pulse rate | Up to 10 kHz (C-scan) |
| data processing | PA channel | UT channel |
| data points | 8192 more | |
| Real time average | 2, 4, 8, 16 | 2, 4, 8, 16, 32, 64 |
| detection | RF, full wave, positive half wave, and negative half wave | |
| filtering | 3 low-pass, 3 band-pass, and 5 high pass filters | 3 low-pass filters, 6 band-pass filters, and 3 high pass filters (8 low-pass filters in TOFD configuration) |
| Video filtering | Smooth (adjusted according to the frequency range of the probe) | |
| The data shows | A-scan refresh rate | Real time: 60 Hz |
|---|---|---|
| data synchronization | According to the internal clock | 1 Hz~10 kHz |
data synchronization |
According to the encoder | Dual axis: 1 step to 65536 steps |
| Programmable Time Correction Gain (TCG) | points | 32: Each focusing rule has a TCG curve. |
| call the police | alarm count | 3 of them |
call the police |
condition | Any logical combination of gates |
call the police |
analog output | 2 |
*The aperture and number of chips of each module model are different. Currently available models are 16:64, 16:128, 32:128, and 32:128PR configurations.
UT2 TOFD module and MXU software
Olympus' new OmniScan MX2 UT2 module embodies a powerful and cost-effective TOFD detection solution. Its improved hardware and software features enable users to use TOFD technology more quickly and conveniently to complete weld inspection. Its signal-to-noise ratio provides excellent data quality for TOFD detection.
Improved features

- TOFD Wizard
- PCS calibration
- Clear B-scan
- Multi TOFD layout
- Direct wave straightening
- Higher PRF in TOFD group
- Higher voltage (up to 340 V) eliminates the need for preamplifiers
These improved features enable faster and easier setup, improve collection and display performance, quantify defects, and thus enhance overall productivity.
Multi TOFD layout
The new multi TOFD layout can display more than one group at a time. This can facilitate the localization and quantification of defect indications by observing the interrelationships between groups.

Direct wave straightening
The straight wave straightening tool provides users with a more coherent display view, making it easier for them to interpret the content in the view. The straight wave straightening function can also evaluate the depth and size of defects.
 Original TOFD data |
 TOFD data after straight wave straightening |
The software improvement features mentioned above have also been integrated into the OmniPC software, allowing users to analyze data on a PC while also being able to re install OmniScan for another data collection operation.
Scanners and accessories

HST Lite TOFD Scanner
The new HST Lite scanner is an excellent choice for single channel TOFD detection that emphasizes signal quality and offers high cost-effectiveness. The combination of the magnetic wheel and the spring-loaded probe bracket provides the scanner with excellent stability required for high-quality single line detection. The scanner can be operated with one hand and can also be attached to ferromagnetic surfaces, even when the scanner body is facing the ground.
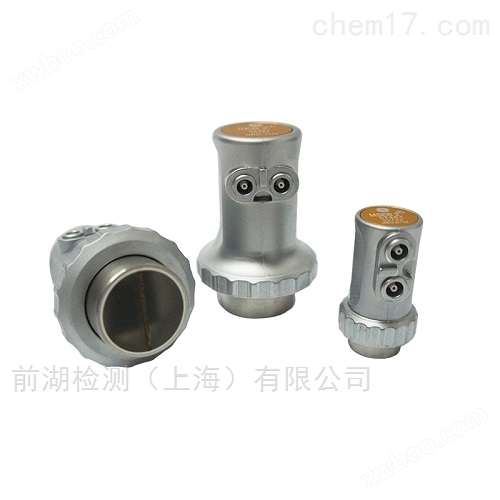
Stainless steel TOFD wedge block
|
The HST Lite purchased as a set comes standard with a new stainless steel TOFD wedge block. These wedges are considered to be a very important upgraded product derived from ordinary Rexolite wedges, and are a better choice for most applications. These wedges have multiple advantageous characteristics:
|
 The new stainless steel wedge (left side) has a shorter contact distance (3 millimeters), which can better cover the weld area. |
These wedges are compatible with Olympus' high-performance TOFD series probes.
Perform TOFD inspection on small pipelines
Another type of TOFD series wedge specially designed for use with mature COBRA scanners can be used for detection applications with narrow operating spaces. These wedges can be used with ST1 probes with a chip diameter of 3 millimeters to inspect pipelines ranging from 1 inch to 4.5 inches in diameter. These wedges have various longitudinal wave refraction angles, and users can order wedges of specific diameters or a wedge set that includes all diameters. |
 The COBRA small diameter pipeline scanner can use appropriate wedges, cables, and probes for TOFD detection. |

Industrial scanner
The ability of industrial scanners to accurately locate probes based on the condition of the tested surface greatly improves the quality of detection. Olympus provides a variety of industrial scanners and accessories for inspectors, providing great assistance for inspection work. The scanner has multiple configurations, in addition to manual and electric configurations, there are also differences between single axis encoding and dual axis encoding.

Weld seam detection solution
Olympus' versatile welding solutions help users effectively complete inspection tasks through the use of multiple technologies and scanning tools. Phased array, time-of-flight diffraction (TOFD), and conventional ultrasound techniques can be used alone or in combination to cover the entire weld area during inspection and achieve high detection rates.

Corrosion detection solution
Olympus has produced various products for a wide range of users, which can manually or automatically detect pipelines and tanks with corroded inner walls, as well as high-temperature surfaces. Corrosion imaging of large-area pressure vessels and stress cracking areas is a typical application that requires manual or automatic detection.

Composite material testing solution
Olympus' composite material testing solutions include powerful and fast portable and integrated testing instruments. Olympus can also provide users with options for detecting various types of composite materials and honeycomb structural components. Ultrasonic and adhesive testing technology, when used in conjunction with specific scanners and probes suitable for different applications, can meet the diverse needs of maintenance or manufacturing industries.

Weld seam detection scanner
Olympus provides users with various scanners to meet their needs for weld seam inspection during manufacturing or maintenance processes. Some scanners can be equipped with multiple probes, which can cover the entire volume of the weld seam with one scan, thus detecting many materials including small-diameter pipelines to flat workpieces. Whether users choose electric or manual scanners, they will be amazed by the universal applicability, independence, and repeatability of these scanners.

Corrosion detection scanner
Corrosion imaging is a highly demanding application that requires the use of a * probe to complete. This probe should have the performance of providing single axis or dual axis encoding positions. This scanner can be installed on pipelines and flat surfaces, making it very convenient to use, and can quickly detect various defects ranging from delamination defects generated during the manufacturing process to thinning of in-service walls.

Aerospace inspection scanner
A major characteristic of aerospace inspection applications is the need for rapid acquisition of C-scans when detecting large areas. The adjusted scanner mainly uses suction cups, which can effectively adhere to the surface of composite materials and perform imaging operations with the help of two additional encoding axes.

Scanner accessories
Olympus provides users with a variety of accessories, such as coupling agent supply devices, pulse generators, and preamplifiers, to help improve data quality, facilitate detection, and enhance detection repeatability.

Weld series probe
The cable of the weld detection probe will extend from the front or top of its casing, which can prevent the cable from winding around the probe holder of the scanner. These probes are suitable for manual and automatic inspection of welds. The A31 and A32 weld series phased array probes and wedges, with their simple design, not only simplify and standardize weld detection, but also improve signal-to-noise ratio.

Wedge block for passive axis focusing (PAF)
This focusing wedge series helps compensate for the divergence of the sound beam in the passive axis direction when detecting circumferential welds in pipelines. A narrower sound beam can quantify shorter defects in the scanning axis direction, thereby helping to reduce scrap rates and provide clearer images.

Double crystal array probe for detecting welds
The dual matrix (DMA) probe consists of two matrix probes connected to the same connector, and has the ability to detect using transmit receive longitudinal wave (TRL) sound beams. This type of probe is particularly useful for detecting pipelines with weld overlay or materials with high attenuation.

Double crystal array probe for corrosion detection
The dual crystal linear array probe provides various advantages over conventional ultrasonic dual crystal probes for corrosion detection applications. This phased array solution can provide larger beam coverage, faster scanning speed, and C-scan imaging with higher data point density, thereby improving detection efficiency.
 new
HTHA probe
In the application of detecting high-temperature hydrogen induced (HTHA) defects, these optimized twin crystal linear array probes and fully focused mode (TFM) probes can provide a wider scanning angle range and extended focusing range, and can also improve the quality of signal response when using higher gains.

Manual contact probe
The A24 probe series used by Olympus for manual contact detection features an ergonomic housing design, with replaceable membranes that provide a larger square aperture, making it suitable for a variety of different applications. A thin film with a thickness of 0.5 millimeters is more convenient for verifying coupling conditions, allowing the probe to move smoothly on rough surfaces and preventing wear and tear.

EdgeFORM
Automakers use EdgeFORM phased array solutions to inspect the bonding or adhesive seams of trucks, engine hoods, and door panels to detect gaps with insufficient bonding or lack of adhesive.

Small bottom probe
The small bottom probe can enter very narrow areas for detection (the bottom size of the A00 probe is 8 × 8 millimeters).

Universal probe
The universal probe combines a thin probe/wedge block together, making it easier to enter small areas for detection. Olympus also offers a variety of wedges for users to choose from, to help them complete various angle beam detection applications. These probes can not only manually or automatically detect thicker welds ranging from 6.35mm to 38mm, but also detect cracks and weld defects in castings, forgings, pipelines, machined parts, and structural components.

Near wall probe
The two ends of the near wall probe have short blind spots (the distance from the center of one chip and the center of the rear chip to the edge of the probe housing close to them is 1.5 millimeters). They are highly suitable for channel detection of composite materials and C-scan detection of composite materials (delamination, debonding, and porosity).

Deep penetration probe
The deep penetration probe can be used in conjunction with various wedges to complete the detection application of sound beams at various angles. These probes are used for deep penetration testing applications, such as detecting thicker plates, welds, forgings, as well as noisy or granular materials.

Water immersion probe
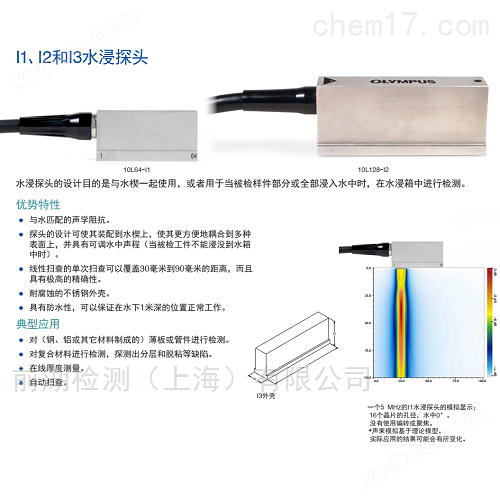
The design purpose of the water immersion probe is to be used in conjunction with a water wedge, or for testing in a water immersion chamber when the tested sample is partially or completely immersed in water. This type of probe belongs to longitudinal wave probes, but after setting, Rexolite wedges can be used for refracted transverse wave detection.

Curved array probe
The housing of the curved array probe is made of corrosion-resistant stainless steel material, which can ensure waterproof performance at a depth of no more than 1 meter underwater. The acoustic impedance of these probes matches the acoustic impedance of water. These probes are compatible with adjustable water immersed wedges, which can not only detect delamination defects in composite materials, but also detect the inner corners of carbon fiber reinforced polymer (CFRP) products.

Water immersed corner wedges for curved array probes
The water immersed corner wedges used for curved array probes have specific radii and angles, and their radii can also be adjusted to be suitable for detecting various workpieces. These wedges are designed for manual scanning and are used in combination with a pocket wheel encoder.

Probe with integrated wedge block and compliant with specifications
This type of probe with an integrated wedge block that meets specifications places the probe and wedge block in the same housing, allowing the combination of the probe and wedge block to have a very thin profile for contact angle beam detection. Since there is no need to use a coupling agent between the probe and the wedge, a good coupling state will always be maintained between the probe and the wedge. These probes can not only manually detect stress corrosion cracks and complete applications that comply with AWS and DGS specifications, but also simultaneously use angles ranging from 40 ° to 70 ° for manual weld seam detection.

Wedge block for angle beam probe
Olympus provides wedges that can generate standard refractive angles of 0 °, 45 °, 55 °, and 60 ° in steel for transverse or longitudinal wave angle beam detection in the range of 30 ° to 70 °. These wedges are equipped with stainless steel screw sockets, which can firmly connect the probe and wedge together. Users can order IHC wedge options to improve the quality of testing. The IHC options include spray holes, mounting holes on wedge frames for connecting Olympus scanners, and hard alloy bars to improve wear resistance.