-
E-mail
1964962058@qq.com
-
Phone
18626328873
-
Address
Dongfang Steel City, Xishan District, Wuxi City
Product Categories
Wuxi Minghongda Metal Products Co., Ltd


Stainless steel 321 rod _ Price trend _ How much does it cost per square meter
NegotiableUpdate on 01/22
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
Stainless steel 321 rod _ Price trend _ How much does it cost per square meter $r $n? Compared with austenitic and ferritic stainless steel for welding, the primary difference lies in the potential hard HAZ martensitic structure and matching composition of the welding metal.
Product Details
Stainless steel 321 rod _ Price trend _ How much does it cost per square meter
Common martensitic alloys, such as 410 type, have moderate chromium content, 12-18% Cr, low Ni, but more importantly, relatively high carbon content. The primary difference between austenitic and ferritic stainless steels and welded stainless steels lies in the potential hard HAZ martensitic structure and the matching composition of the welded metal. The data can be successfully welded, providing prevention methods to prevent cracking in the heat affected zone, especially for thick walled components and highly constrained joints.
Fundamentally, stainless steel with white spots is qualified in terms of heavy metal policies. The formation of white spots may be due to the modification of the protective film on the surface of the stainless steel by acid solution, resulting in defects, pores, or salt formation on the surface of the stainless steel plate; Dark rust spots are iron oxides formed by severe corrosion of iron in stainless steel. The above two types of stains are generally difficult to remove, and even if sandpaper is used to remove them, they will regenerate after a period of time. The main cause of stainless steel rusting is usually due to the iron contained in the steel. However, as long as there is an oxide protective film on the surface of the stainless steel material, the iron will not be exposed to the air, and in this situation, stainless steel will not rust easily.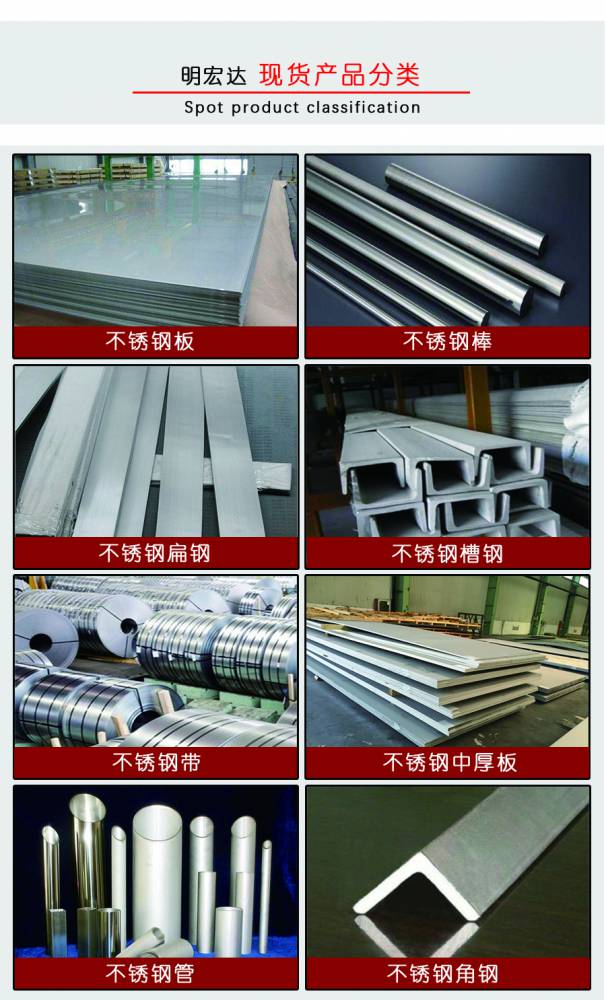
Stainless steel 321 rod _ Price trend _ How much does it cost per square meter
The high hardness in HAZ makes this type of stainless steel very prone to hydrogen cracking. The danger of general cracking increases with the carbon content. The necessary precautionary measures to reduce the risk include: using low hydrogen processes (TIG or MIG) and ensuring that consumables for flux or flux coating are monotonous according to the manufacturer's instructions (MMA and SAW); Preheat to around 200 to 300 degrees Celsius. C. The actual temperature depends on the welding process, chemical composition (especially Cr and C content), cross-sectional thickness, and the amount of hydrogen entering the weld metal; Adhere to the recommended low inter road temperature.
Perform post weld heat treatment, such as at 650-750 ℃. The timing and temperature will be recognized by the chemical composition. Thin low-carbon materials below 3mm can generally be welded without preheating, using low hydrogen technology, with low binding of the joint, and paying attention to cleaning the joint area. Thicker parts and higher carbon content (>0.1%) may require preheating and post weld heat treatment. Immediately after welding, post weld heat treatment is carried out, which not only requires tempering (toughening) treatment of the structure, but also disperses hydrogen from the weld metal and heat affected zone.
Similar Product Recommend
